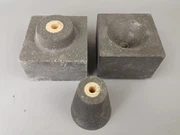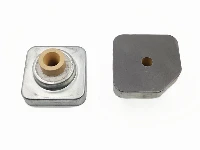
How to confirm bore size of zirconia metering nozzle?
Nov 07, 2026
The bore size of zirconia metering nozzle directly decides molten steel flow rate and casting speed during continuous casting. Wrong bore size will lead to speed fluctuation, overflow or break-out risk. Steel mills and refractory buyers need standard methods to verify this dimension before installation.
1. Check original drawing and order sheet first
Start with the technical drawing provided by the supplier. The nominal bore diameter is marked on the drawing. Cross check the drawing data with your purchase order. Confirm the marked size matches the technical requirement of your continuous caster. Note the tolerance range agreed at the time of order.
2. On-site dimension measurement
Use internal caliper or optical measuring instrument to test the inner hole. Measure at three positions: inlet end, middle section and outlet end of the nozzle. Record all readings. If the nozzle has a taper structure, the diameter will differ from top to bottom. Do not only measure one single point.
Measurements should be taken at room temperature. High temperature will change the dimension, so hot state measurement is not used for incoming inspection.
3. Match with casting process parameters
Flow rate of molten steel depends on bore size, steel temperature and tundish liquid level. You can calculate the theoretical flow according to your target casting speed. If the measured bore falls outside the calculated range, this nozzle cannot be used for this production batch.
Different steel grades also set limits on available bore size. Aluminum killed steel requires stricter size control to reduce clogging.
4. Distinguish nominal size and actual size
Nominal bore size is the reference number for ordering. Actual finished size sits within the tolerance zone. Both parties need to confirm acceptable tolerance before production. Some users only focus on nominal size and ignore tolerance, which causes inconsistency in casting performance.
5. Sample test before mass use
For new orders or new size specifications, run a small trial first. Install the nozzle and track the real casting speed. If the actual speed cannot reach the target value, recheck the bore dimension again. Adjust the specification for next production if needed.
Common mistakes to avoid
- Only check the outer diameter and skip inner bore measurement
- Confuse inlet diameter with outlet diameter on tapered nozzles
- Ignore dimension change after long time storage or rough handling
- Use measuring tools without calibration
Changtai provides dimension inspection report together with zirconia metering nozzles. All finished nozzles go through bore size checking before delivery. Send us your caster parameters if you need support on size selection.